Material Choice Is the Safety Line
Glass, Steel or Plastic — What Each One Fails At
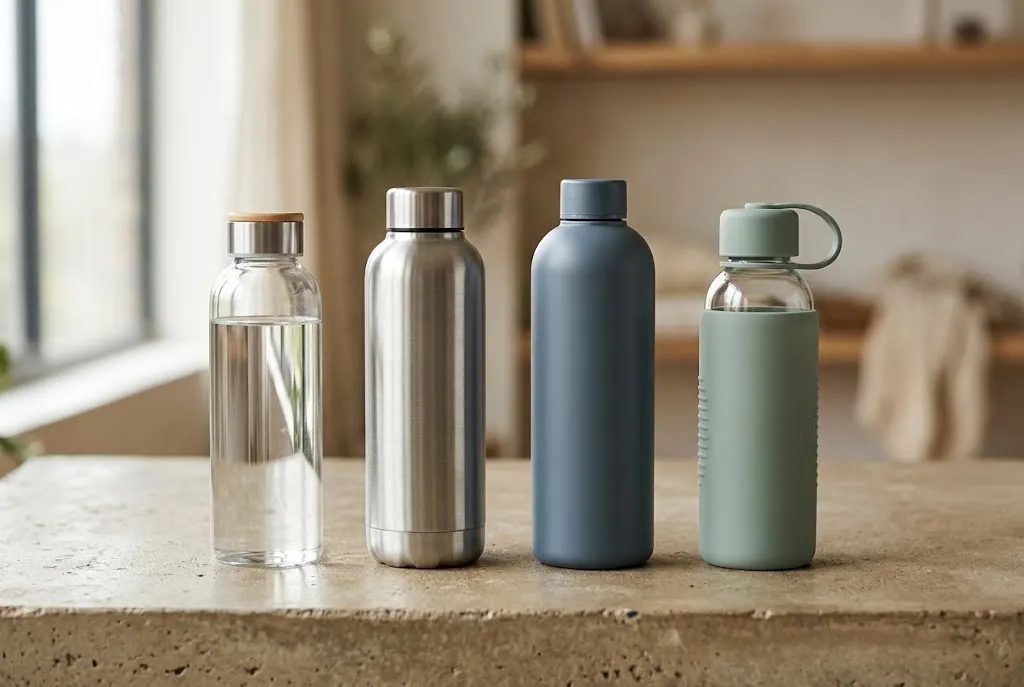
Table of Contents
- 1. The “Exploding Bottle” Is a Material Decision, Not Bad Luck
- 2. Four Material Families, Four Different Safety Logics
- 3. Glass: Thermal Shock and How It Fails
- 4. Stainless Steel: Grade, Leaching and the Substitution Risk
- 5. Plastic: BPA, Its Replacements, and the Regulatory Shift
- 6. Silicone, Seals and the Parts Nobody Specifies
- 7. Coatings, Inks and the Decoration Safety Layer
- 8. Compliance Documents by Market: What to Actually Request
- 9. A Buyer’s Material Safety Checklist
- 10. Partner With Mofecup on Material Specification
1. The “Exploding Bottle” Is a Material Decision, Not Bad Luck
Most people have seen it happen, or know someone who has. Hot tea or boiling water goes into a glass bottle, there is a sharp crack, and the glass either splits cleanly or shatters outright.
The natural assumption is a manufacturing defect or plain bad luck. In most cases it is neither. It is the predictable outcome of a material decision made long before the bottle reached the customer — a decision about which glass, which steel grade, which plastic, and which seal was specified on the purchase order.
This is why material selection deserves a different status in B2B drinkware sourcing than colour, finish or logo method. Those are brand decisions and can be revised late. Material is a safety and liability decision, and it is the hardest thing to change after tooling. A material failure produces outcomes that no amount of good quality control downstream can undo:
- User injury risk — the only failure mode in this industry that escalates beyond money
- Reviews and refunds across an entire batch, not a single unit
- Regulatory exposure where a material or coating does not meet the requirements of the destination market
- Long-term credibility damage — hardest to rebuild, because it was avoidable
The rest of this article treats material choice the way a sourcing team should: as a question of what each material is permitted to do, and what it does when you push past that limit.
2. Four Material Families, Four Different Safety Logics
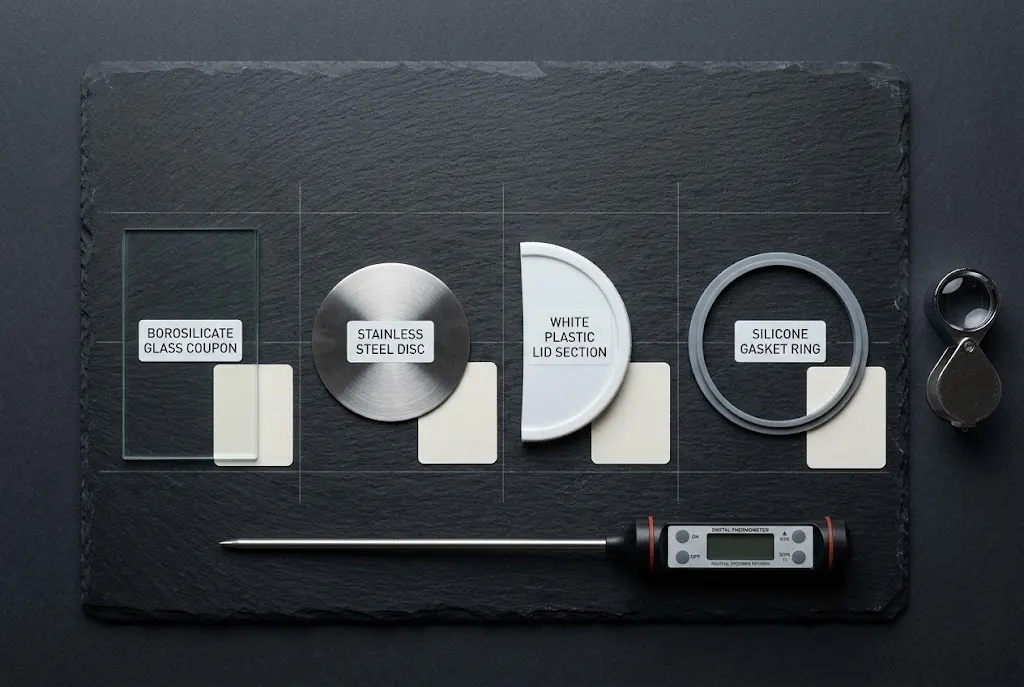
A drinkware bottle is almost always assembled from more than one material — a body, a lid, a seal, often a coating and a printed layer. Each family carries its own risk profile, and the risks do not substitute for one another. This is the single most useful table in the article, because it tells you which question to ask about which component.
| Material family | What the safety question really is | Characteristic failure | Main document to request |
|---|---|---|---|
| Glass | How much thermal shock can it take before it fractures? | Cracking or shattering under sudden temperature change | Glass type and thermal shock rating |
| Stainless steel | Which alloy grade, and can it be proven to be that grade? | Pitting corrosion and metal ion release; grade substitution | Material test certificate and composition report |
| Plastic (body, lid, liner) | Which polymer, and what does it release over time and heat? | Additive migration; opacity and microfracture with age and washing | Polymer identification plus migration testing |
| Silicone and elastomer seals | Is it genuinely silicone, and is it food-contact grade? | Odour and taste transfer; hardening or tackiness with heat cycling | Food-contact declaration for the specific compound |
Two consequences follow immediately. First, approving one certificate does not approve the product — a stainless body, a PP lid and a silicone gasket are three separate compliance conversations. Second, the highest-risk component is often not the one buyers examine most. Everyone looks at the bottle body. The seal and the coating are where a surprising share of problems originate. For a material-by-application mapping across all of these, see our guide to drinkware materials by application.
3. Glass: Thermal Shock and How It Fails
Glass has the narrowest safety margin of the four families, and the reason is arithmetic rather than opinion. Its behaviour under heat is governed by the coefficient of linear thermal expansion — how much the material grows per degree of temperature rise. When one part of a bottle heats faster than another, the difference in expansion creates internal stress, and glass relieves stress by cracking.
| Property | High borosilicate glass | Ordinary soda-lime glass |
|---|---|---|
| Coefficient of linear thermal expansion | ≈ 3.3 × 10⁻⁶ / K | ≈ 9 × 10⁻⁶ / K |
| Thermal shock resistance | High — takes boiling water directly | Low — high risk of cracking |
| Optical appearance | Clear, neutral tone | Often a green or blue edge tint |
| Chemical behaviour | Highly inert — no odour or taste transfer | Less stable; can interact with contents |
| Failure behaviour | Better internal stress balance; tends to fail in larger, blunter fragments | More prone to sudden, finer fragmentation |
Two things are worth being precise about, because both are commonly overstated in supplier marketing.
First, “borosilicate” is not synonymous with unbreakable. No glass is. The advantage is that borosilicate expands roughly three times less than soda-lime, which buys a much wider tolerance to sudden temperature change before stress accumulates — nothing more. Dropped, twisted or thermally cycled past its limit, it still breaks.
Second, “borosilicate” is a family, not a spec. The number that defines the safety margin is the expansion coefficient — commonly quoted in the region of 3.3 × 10⁻⁶ / K for the high-borosilicate type used in laboratory glassware — and a supplier should be able to state the value for the actual body they supply. “Borosilicate” written on a quotation without a coefficient allows the margin to drift without anyone noticing.
Going deeper on glass specificallyThis article stays at the decision level across all four material families. For a full technical comparison of the two glass types — thermal curves, mechanical strength, chemical resistance, cost behaviour at volume, decoration compatibility and application recommendations — see our dedicated guide: Borosilicate vs soda-lime glass for custom drinkware.
4. Stainless Steel: Grade, Leaching and the Substitution Risk
Stainless steel has the widest safety margin of the four families — which is exactly why it is also the family where the specification can quietly go wrong without any appearance change. Two bottles can be visually identical, feel identical, and behave identically in the hand, while one is 304 and the other is a cheaper alloy substituted at the coil stage.
The safety logic is compositional. Austenitic stainless steel is defined by alloy content, and those ranges come from material specifications rather than from marketing[1]. The step that matters for acidic drinks is the addition of a small amount of molybdenum, which is what separates 316 from 304 and what substantially improves resistance to localised pitting corrosion. Grade 201, which substitutes manganese for much of the nickel, costs less and corrodes sooner — a legitimate choice for non-food-contact promotional items, and a poor one for anything holding citrus, tea or electrolyte drinks.
| Grade | Safety position | Sensible use |
|---|---|---|
| 201 | Lower corrosion resistance, higher manganese content — the grade behind most grade-substitution problems | Only where there is no food contact |
| 304 (“18/8”) | Accepted food-contact standard; good for water and neutral drinks | Standard bottles, tumblers, volume programmes |
| 316 / 316L | Widest margin; molybdenum resists chloride and acid pitting. Low-carbon 316L additionally protects weld-adjacent zones | Tea, coffee, juice, sports drinks, kids’ and premium ranges |
Because the difference is invisible, the only real safety control is verification: a material test certificate tied to the batch actually shipped, and XRF composition reading where the value of the order justifies it. A certificate covering the material batch rather than each individual bottle is normal practice — the control is to insist on one for every shipment rather than the first.
For the full compositional and verification picture, including the four checks that catch a substituted grade, see 201 vs 304 vs 316 stainless steel compared. If the specific question is whether the 316 premium pays for itself in your programme, that cost model is worked through in is the 316 upgrade worth it. And for what acceptable metal release into a drink actually looks like, see heavy metal leaching in drinkware and our notes on stainless steel safety for drinking.
5. Plastic: BPA, Its Replacements, and the Regulatory Shift
Plastic is the family where the regulatory ground has moved most in the last few years, and where a specification written three years ago may no longer be defensible. This is not a hypothetical risk for a brand: it is the category most likely to require a packaging or material change mid-programme.
Bisphenol A is the clearest example. In April 2023, EFSA published a re-evaluation of BPA used in food-contact materials and significantly reduced the tolerable daily intake compared with its previous assessment[6]. On 19 December 2024 the European Commission adopted a ban on the use of BPA in food-contact materials[6] — a step change from “restrict the migration level” to “do not use the substance”. Any B2B drinkware programme selling into the EU, or planning to, needs to know where its components sit against that.
| Polymer | Typical position | What to verify |
|---|---|---|
| Polycarbonate (PC) | Historically common for clear, tough bottles; BPA-based. Increasingly problematic in food-contact applications | Whether it is still permissible in each destination market |
| Tritan and other BPA-free copolyesters | The usual replacement for PC; clarity and impact resistance without BPA as a monomer | That the grade is food-contact approved for the intended use and temperature |
| Polypropylene (PP) | Widely used for lids, caps and liners; heat tolerant and well established | Colourant and additive package, not just the base polymer |
| PET / rPET | Common in single-use and lightweight formats | Recycled content sourcing and the documentation behind recycled streams |
Three practical points for a sourcing team. “BPA-free” is a claim that requires evidence, and the evidence attaches to the specific component rather than to the product as a whole — a BPA-free body with an undocumented liner has not been established as BPA-free. Our notes on BPA material safety testing cover how that is documented.
Second, replacing a substance is not the same as removing a risk. A substitution removes a named hazard; whether the replacement carries its own concerns is a question the buyer should ask rather than assume. Third, mechanical ageing matters independently of chemistry. A plastic that clouds, crazes or microfractures with washing and use releases more material than a new one, whatever it is made of — which is why migration testing is specified on aged or conditioned samples, not fresh ones. Our comparisons of Tritan vs polypropylene vs polycarbonate and glass vs Tritan vs PP cover the trade-offs between these options, and microplastic contamination in plastic bottles addresses the ageing question directly.
6. Silicone, Seals and the Parts Nobody Specifies
The gasket is a small component with a disproportionate effect on both safety and customer experience. It is also the component most often left unspecified — the buyer approves a body material and a lid colour, and the seal arrives as whatever the factory used that week.
Three things are worth pinning down:
- Material, not the word “silicone”. The relevant specification is the compound and its food-contact approval, not the family name. Cheap elastomer substitutes look and feel similar when new and behave differently after heat cycling.
- Odour and taste at temperature. A seal that is acceptable cold can transfer odour or taste to hot liquid. Ask for the odour and taste assessment, not only the migration figures.
- Behaviour over the product’s life. Seals harden, soften or become tacky with repeated washing and heat. A gasket that stops sealing is a leak; on a hot-filled bottle, a leak is a burn risk. Durability here is a safety property, not a convenience one.
The same discipline applies to sleeves and grips, which are contact-relevant components rather than accessories: a silicone sleeve sits against the body and against the user’s hand all day. Our guide to food-grade silicone in gaskets, straws and seals covers the specifications to write into a purchase order, and material hygiene in reusable bottles deals with the cleaning and bacterial side of the same parts.
7. Coatings, Inks and the Decoration Safety Layer
Decoration is where brands focus their attention and where compliance is most often overlooked, because a coating is not the substrate. A perfectly specified 304 body with an undocumented interior coating has an unverified interior.
The principle is straightforward: the further decoration sits from the drink, the lower its food-contact significance — and the closer it sits, the more it matters.
| Decoration | Food-contact significance | What to request |
|---|---|---|
| Exterior laser engraving | Low — removes surface material, adds none | Confirmation no coating is breached through to the substrate |
| Exterior screen print / decal | Low — outside the vessel | Ink and carrier compliance plus dishwasher durability |
| Exterior powder coat / PVD | Low, but chips and flaking matter | Abrasion and adhesion test data, not just the colour |
| Interior coating / liner | High — sits directly against the drink | Full migration testing on the finished, decorated article |
| Colourants and masterbatch | High in plastic components — additives migrate | Additive declaration, not just the base polymer name |
Functionally, coatings and adhesives on a food-contact article are regulated as their own category rather than as part of the substrate[2], and plastic components such as lids and seals fall under their own part of the same framework[3]. The consequence for a specification document is simple: the bill of materials has to be treated as a list of separate regulatory items, not as one product with one certificate. For how migration testing is actually performed on finished drinkware, see food-contact migration testing.
8. Compliance Documents by Market: What to Actually Request
Compliance obligations follow the market you sell into, not the country of manufacture. The table below sets out the framework that applies and the document that discharges it — which is the part a purchase order actually needs.
| Market | Framework | Document to request |
|---|---|---|
| United States | FDA food-contact framework for substances used in materials that contact food[5] | Composition or migration statement covering each food-contact component, with a regulatory status basis |
| European Union | Regulation (EC) No 1935/2004 — framework for food-contact materials[4]. Bisphenol A banned in food-contact materials as of 19 December 2024[6] | Declaration of compliance, plus confirmation that no bisphenol A is used in any component |
| EU — specific substance regimes | Substance-level restrictions on food-contact materials, including PFAS-related restrictions | Component-level statement for coatings and non-stick or water-repellent treatments |
| China (and as a factory baseline) | GB 4806 series — national food safety standards for food-contact materials, including GB 4806.9 for metals[7]; GB/T 29606 for stainless steel drinkware[8] | Test reports naming the standard, the method and the article tested |
| California, USA | Proposition 65 — separate exposure-disclosure regime that applies on top of federal rules[9] | Lead (and other listed substance) content or exposure assessment for decorated items |
| All markets | Material specification of the grades supplied[1] | Material test certificate per batch, traceable to the shipment |
Two rules make this manageable. First, ask for documents against a named standard, not against a word. “Food-grade”, “medical-grade” and “BPA-free” are claims; a report naming a standard, a test method and the article tested is evidence. Second, ask for the full bill of materials. A supplier who can only document the body has documented a third of the product. For the certification language that is defensible on packaging, see our guide to food-grade certification standards, and for the European substance regimes specifically, REACH and RoHS compliance testing and PFAS/PFOA-free compliance.
9. A Buyer’s Material Safety Checklist
Nine questions, answerable before the purchase order. If a supplier cannot answer most of them in writing, the specification is not yet controlled — regardless of how good the sample looks.
- What is the material, specified precisely? Glass type and expansion coefficient; steel grade; polymer grade — not “glass”, “stainless” or “plastic”.
- What is the failure mode, and at what limit? Thermal shock range for glass, pitting conditions for steel, temperature and ageing limits for polymers.
- Is the material documentation batch-traceable? A certificate for the prototype does not cover the production run.
- Have all non-body components been specified — lid, seal, straw, sleeve, interior coating?
- Is migration testing on the finished, decorated article — not on the raw material alone?
- Has the product been tested after ageing or repeated washing? This is where plastic and seal performance actually diverges.
- Do any components contain substances restricted in your destination market — bisphenol A being the live example in the EU?
- Can the supplier name the standard each report references, and the laboratory that issued it?
- Would you be comfortable defending this specification to a retail buyer or a market surveillance authority? If not, the gap is the specification, not the paperwork.
One framing to keep. Material choice is not a technical detail that a supplier handles on the brand’s behalf. It is the point at which the brand decides which risks it is willing to own — and it is almost always cheaper to make that decision on a quotation than after a recall.
Specifying a bottle and want the material side handled properly?Mofecup supplies custom water bottles in borosilicate glass, 304/316 stainless steel and food-contact polymers, and will quote the material documentation alongside the unit price. Tell us the drink, the temperature range, the destination market and the volume, and we will come back with a specification and the documents that support it. Request a quote →
10. Partner With Mofecup on Material Specification
Mofecup is not positioned as a glass factory, a steel mill or a polymer producer — and we are deliberate about that. Our role is to define the correct material standard for your use case, then make sure it is executed consistently across qualified manufacturing partners and that the documentation holds up.
In practice, that means:
- Material standard defined first — expansion coefficient, steel grade or polymer grade chosen against your drink, temperature range and market.
- Borosilicate glass with controlled production — high-temperature melting and precision annealing, the step most often rushed in low-cost production and the one that decides whether internal stress is released.
- 304 or 316 stainless steel with composition verification, so a 316 specification is genuinely 316.
- Full bill-of-materials specification — lid, seal, straw, sleeve and any interior coating treated as separate regulatory items rather than as accessories.
- Compliance documentation per market, covering the assembly as sold, with test reports traceable to the production batch.
- Decoration that survives the dishwasher — borosilicate bodies take high-temperature printing and durable coatings, so the logo is still there in year two. See materials by application for how this maps to end uses.
- Capacity and wall options — including thicker bodies and protective sleeves where impact resistance matters, and sleeve combinations for outdoor use.
Explore the material comparisons behind these recommendations, or send your brief with the drink, temperature range, market and volume and we will respond with a specified, costed option.
Footnotes & References
[1] ASTM International. ASTM A240/A240M — Standard Specification for Chromium and Chromium-Nickel Stainless Steel Plate, Sheet, and Strip for Pressure Vessels and for General Applications (source of the type 201, 304 and 316 composition ranges referenced above). astm.org
[2] U.S. Electronic Code of Federal Regulations. 21 CFR Part 175 — Indirect Food Additives: Adhesives and Components of Coatings. ecfr.gov
[3] U.S. Electronic Code of Federal Regulations. 21 CFR Part 177 — Indirect Food Additives: Polymers (applies to plastic components such as lids, seals and gaskets). ecfr.gov
[4] European Parliament and Council. Regulation (EC) No 1935/2004 on materials and articles intended to come into contact with food. eur-lex.europa.eu
[5] U.S. Food & Drug Administration. Packaging & Food Contact Substances (FCS) — regulatory framework for substances used in materials that contact food. fda.gov
[6] European Food Safety Authority (EFSA). Bisphenol A and other bisphenols — EFSA’s April 2023 re-evaluation of BPA in food-contact materials, and the European Commission’s ban on the use of BPA in food-contact materials adopted on 19 December 2024 under Commission Regulation (EU) 2024/3190. efsa.europa.eu
[7] National Health Commission of the People’s Republic of China. GB 4806 series — National food safety standards for materials and articles in contact with food; GB 4806.9 covers metal materials and products for food contact (食品安全国家标准 · 食品接触用金属材料及制品), current edition GB 4806.9-2023. chinesestandard.net
[8] Standardization Administration of China. GB/T 29606 — Stainless steel vacuum cups (不锈钢真空杯). Current edition GB/T 29606-2013; revised edition GB/T 29606-2026 published January 2026 for implementation February 2027. openstd.samr.gov.cn
[9] California Office of Environmental Health Hazard Assessment (OEHHA). Proposition 65 — Safe Drinking Water and Toxic Enforcement Act. oehha.ca.gov